Adam Ferneyhough, UK Country Manager at DAB Pumps, looks at what goes into a quality pump.
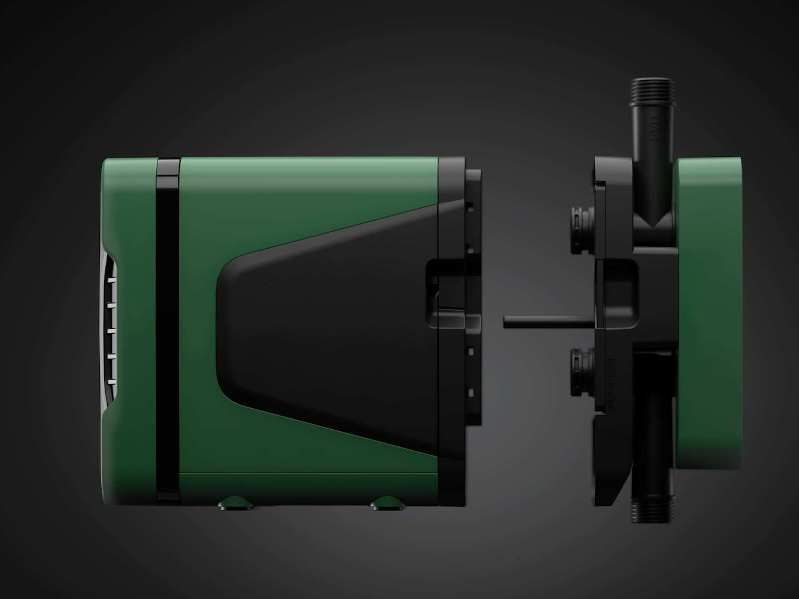
Look at any pump and you would be forgiven for thinking they generally look the same. But often, the difference lies beneath the surface. It’s not just about the outer casing, it’s about the internal workings, the precision engineering, and the technology that drives the system.
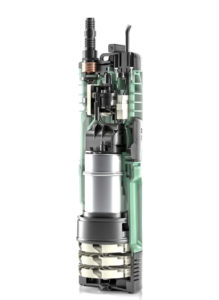 Take a look at the cut-away of the Divertron, a submersible cold water automatic pressure booster pump that combines the pump, electronic control and automatic operation into a single unit. As with all quality pumps, it’s what’s inside that makes the difference.
Designed for use in wells, rainwater harvesting systems, tanks and cisterns, the Divertron automatically starts and stops in response to water demand, maintaining a dependable supply for domestic use, garden irrigation and light pressure boosting applications. By integrating the electronic control system within the pump, it removes the need for separate external controllers, helping installers achieve a quicker, cleaner installation while reducing the number of components on site.
Precision-engineered hydraulic components, durable materials and intelligent electronic controls work together to deliver dependable performance, minimise maintenance and provide years of reliable operation. For installers, that means greater confidence that the job will perform as expected long after they’ve left site.
 Compact Pumps
The domestic market is also driving another significant trend: smaller, quieter pumps that can be installed inside the home without compromising on performance. As modern homes continue to shrink plant room space – and homeowners increasingly expect systems to be discreet – compact booster sets have become an attractive solution for installers.
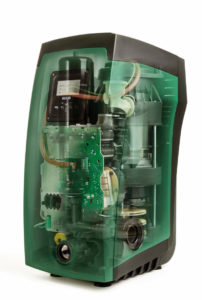
The DAB Esybox Pop has been developed specifically for these applications. Its compact footprint makes it ideal for boosting water pressure in houses and apartments where space is at a premium, while its low operating noise means it can be installed in utility rooms or other occupied spaces without becoming a nuisance. For families struggling with poor shower performance or inconsistent pressure at multiple outlets, a compact booster such as the Esybox Pop can transform day-to-day living by delivering consistent water pressure throughout the home.
Compact size is only part of the story. Pumps are becoming increasingly intelligent, giving installers greater visibility during commissioning and maintenance while offering homeowners more control over their systems. DAB’s H2D app enables compatible pumps to be monitored and managed from a smartphone, providing quick access to operating information, performance data and system settings. This not only simplifies commissioning but can also support faster diagnostics should an issue arise.
The NG Panel builds on this connected approach, providing an intuitive interface for system setup, monitoring and management. Together with the H2D app, it demonstrates how modern pumping solutions are becoming smarter and more connected with both installers and homeowners. As expectations around connected homes continue to grow, intelligent pump technology is becoming just as important as hydraulic performance.
Scaling Up
For larger residential or commercial projects, the demands are higher, but the principles of quality remain the same. The Esybox Max is our integrated pumping system designed for these exact scenarios. Looking at its internal structure, you can see the robust electronic vertical multi-impeller pump, the advanced display, and the Wi-Fi module.
Esybox Max also features a modular design. The support base (Esydock) and wireless communication between the pumps mean you can easily assemble single, double, triple, or even quadruple systems directly on-site. This O.S.A. (On Site Assembly) concept is a game-changer. It means one person can often handle an installation that would typically require a team, saving time and reducing labour costs.
The Esybox Max also utilises a water-cooled permanent magnet motor. This choice of material and cooling method makes the pump incredibly quiet, a crucial factor when installing in residential buildings where noise can be a nuisance.
Manufacturing
The quality of a pump is intrinsically linked to how it’s made. Our manufacturing facilities in Italy are a testament to this. We produce over two million items annually and each one must meet our exacting standards. It’s this dedication to quality control that ensures when you install a DAB pump, you’re installing a product built to last.
So, why does all this matter to installers? Because a quality pump is an investment in your business. When you choose a pump with superior internal components, like those found in the Esybox line, you’re choosing reliability. You’re reducing the risk of breakdowns, which means fewer emergency callouts and more time to focus on new jobs.
Images: DAB Pumps